| Standard | ASTM A672/A672M |
| Material | Carbon or alloy steel |
| Process | EFW (Electric-Fusion-Welded) |
| Grade | A45, A50, A55, B60, B65, B70, C55, C60, C65, C70, D70, D80, H75, H80, J80, J90, J100, L65, L70, L75, N75 |
| Class | 10, 11, 12, 13, 20, 21, 22, 23, 30, 31, 32, 33, 40, 41, 42, 43, 50, 51, 52, 53 |
| Dimension | 16 in. or large |
| Application | High-pressure service at moderate temperatures |
What is ASTM A672/A672M LSAW Steel Pipe?
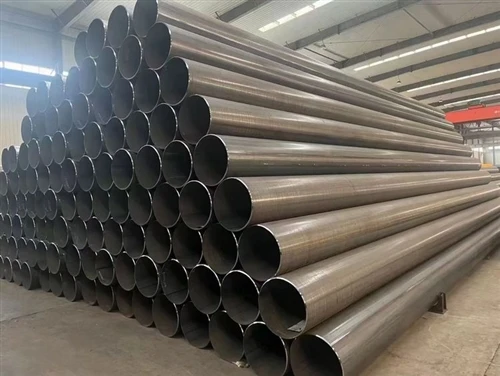
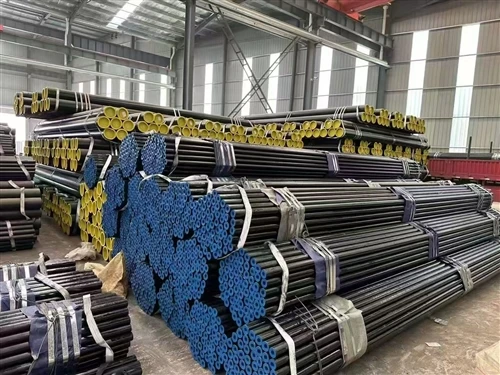
ASTM A672 LSAW Steel Pipe is an electric-fusion-welded steel pipe manufactured from pressure-vessel-quality carbon steel or alloy steel plate for pressure serviceat moderate temperatures. Produced by longitudinal welding, ASTM A672 pipe is suitable for large-diameter pressure piping where controlled material properties, weld quality, non-destructive examination, and hydrostatic testing are important.
Our ASTM A672 LSAW Steel Pipe can be supplied in different grades, classes, outside diameters, wall thicknesses, lengths, and end configurations according to the applicable ASTM specification and project requirements.


Grade Classification
The grade indicates the steel plate used, which determines the chemical composition and mechanical properties of the pipe.
| Pipe Grade | Type of Steel | ASTM Specification | |
| No. | Grade | ||
| A45 | plain carbon | A285 | A |
| A50 | plain carbon | A285 | B |
| A55 | plain carbon | A285 | C |
| B60 | plain carbon, killed | A515 | 60 |
| B65 | plain carbon, killed | A515 | 65 |
| B70 | plain carbon, killed | A515 | 70 |
| C55 | plain carbon, killed, fine-grain | A516 | 55 |
| C60 | plain carbon, killed, fine-grain | A516 | 60 |
| C65 | plain carbon, killed, fine-grain | A516 | 65 |
| C70 | plain carbon, killed, fine-grain | A516 | 70 |
| D70 | manganese-silicon, normalized | A537 | CL-1 |
| D80 | manganese-silicon, Q&TA | A537 | CL-2 |
| H75 | manganese-molybdenum, normalized | A302 | A |
| H80 | manganese-molybdenum, normalized | A302 | B, C or D |
| J80 | manganese-molybdenum, Q&T A | A533 | Cl-1 B |
| J90 | manganese-molybdenum, Q&T A | A533 | Cl-2 B |
| J100 | manganese-molybdenum, Q&T A | A533 | Cl-3 B |
| L65 | molybdenum | A204 | A |
| L70 | molybdenum | A204 | B |
| L75 | molybdenum | A204 | C |
| B, C, or D | manganese-silicon | A299 | A |
|
A: Q&T = quenched and tempered; |
|||
The selection of materials should be made with attention to the temperature of the service. Specification ASTM A20 may be consulted for such guidance.
Class Classification & Heat Treatment
In engineering projects related to ASTM A672, grades are used to specify a set of operations that must be conducted before delivery. This is the case for the common CL22 and CL12.
These operations include whether heat treatment is required, whether the welds need a radiographic inspection and whether pressure testing is necessary.
| Class | Heat treatment on pipe | Radiography, see note: | Pressure test, see note: |
| 10 | none | none | none |
| 11 | none | 9 | none |
| 12 | none | 9 | 8.3 |
| 13 | none | none | 8.3 |
| 20 | stress relieved, see 5.3.1 | none | none |
| 21 | stress relieved, see 5.3.1 | 9 | none |
| 22 | stress relieved, see 5.3.1 | 9 | 8.3 |
| 23 | stress relieved, see 5.3.1 | none | 8.3 |
| 30 | normalized, see 5.3.2 | none | none |
| 31 | normalized, see 5.3.2 | 9 | none |
| 32 | normalized, see 5.3.2 | 9 | 8.3 |
| 33 | normalized, see 5.3.2 | none | 8.3 |
| 40 | normalized and tempered, see 5.3.3 | none | none |
| 41 | normalized and tempered, see 5.3.3 | 9 | none |
| 42 | normalized and tempered, see 5.3.3 | 9 | 8.3 |
| 43 | normalized and tempered, see 5.3.3 | none | 8.3 |
| 50 | quenched and tempered, see 5.3.4 | none | none |
| 51 | quenched and tempered, see 5.3.4 | 9 | none |
| 52 | quenched and tempered, see 5.3.4 | 9 | 8.3 |
| 53 | quenched and tempered, see 5.3.4 | none | 8.3 |
Note: The references in this table are listed below to make them easy to find when you need them.
Heat Treatment
5.3.1 Classes 20, 21, 22, and 23 pipes shall be uniformly heated within the post-weld heat-treatment temperature range indicated in Table 2 for a minimum of 1 h/in. [0.4 hr/cm] of thickness or 1 h, whichever is greater.
5.3.2 Classes 30, 31, 32, and 33 pipes shall be uniformly heated to a temperature in the austenitizing range and not exceeding the maximum normalizing temperature indicated in Table 2 and subsequently cooled in air at room temperature.
5.3.3 Classes 40, 41, 42, and 43 pipe shall be normalized in accordance with 5.3.2. After normalizing, the pipe shall be reheated to the tempering temperature indicated in Table 2 as a minimum and held at temperature for a minimum of 1/2 h/in. [0.2 hr/cm] of thickness or 1/2 h, whichever is greater, and air-cooled.
5.3.4 Classes 50, 51, 52, and 53 pipes shall be uniformly heated to a temperature in the austenitizing range, and not exceeding the maximum quenching temperature indicated in Table 2 and subsequently quenched in water or oil. After quenching the pipe shall be reheated to the tempering temperature indicated in Table 2 as a minimum and held at temperature for a minimum of 1/2 h/in. [0.2 hr/cm] of thickness or 1/2 h. whichever is greater, and air-cooled.
8.3 Pressure Test – Classes X2 and X3 pipe shall be tested in accordance with Specification A530/A530M, Hydrostatic Test Requirements.
9 Radiographic Examination – The full length of each weld of Classes X1 and X2 shall be radiographically examined in accordance with and meet the requirements of the ASME Boiler and Pressure Vessel Code, Section VIII, paragraph UW-51.
| Pipe grade | Post-weld heat treatment temperature range °F (°C) | Normalizing temperature, max, °F (°C) | Quenching temperature, max, °F (°C) | Tempering temperature, min, °F (°C) |
|---|---|---|---|---|
| A 45 | 1100-1250 (590-680) | 1700 (925) | … | … |
| A 50 | 1100-1250 (590-680) | 1700 (925) | … | … |
| A 55 | 1100-1250 (590-680) | 1700 (925) | … | … |
| B 60 | 1100-1250 (590-680) | 1750 (950) | … | … |
| B 65 | 1100-1250 (590-680) | 1750 (950) | … | … |
| B 70 | 1100-1250 (590-680) | 1750 (950) | … | … |
| C 55 | 1100-1250 (590-680) | 1700 (925) | 1650 (900) | 1200 (650) |
| C 60 | 1100-1250 (590-680) | 1700 (925) | 1650 (900) | 1200 (650) |
| C 65 | 1100-1250 (590-680) | 1700 (925) | 1650 (900) | 1200 (650) |
| C 70 | 1100-1250 (590-680) | 1700 (925) | 1650 (900) | 1200 (650) |
| D 70 | 1100-1250 (590-680) | 1700 (925) | … | … |
| D 80 | 1100-1250 (590-680) | … | 1650 (900) | 1200 (650) |
| H 75 | 1100-1250 (590-680) | 1800 (980) | … | 1100 (590) |
| H 80 | 1100-1250 (590-680) | 1800 (980) | … | 1100 (590) |
| J 80 | 1100-1250 (590-680) | … | 1800 (980) | 1100 (590) |
| J 90 | 1100-1250 (590-680) | … | 1800 (980) | 1100 (590) |
| J 100 | 1100-1250 (590-680) | … | 1800 (980) | 1100 (590) |
| L 65 | 1100-1200 (590-650) | … | … | … |
| L 70 | 1100-1200 (590-650) | … | … | … |
| L 75 | 1100-1200 (590-650) | … | … | … |
| N 75 | 1100-1200 (590-650) | 1700 (925) | … | … |
Dimension Tolerance
| Dimension | Tolerance |
| Outside Diameter | Based on circumferential measurement ±0.5% |
| Out-of-Roundness | Difference between major and minor outside diameters, 1% |
| Alignment | Using a 10 ft [3 m] straight edge placed so that both ends are in contact with the pipe, 1/8 in. [3 mm] |
| Thickness | Not more than 0.01 in. [0.3 mm] under the specified nominal thickness |
| Lengths | 0-+0.5in. [0-+13mm] of that specified |
What We Can Supply?
Brisk Steel Factory manufactures ASTM A672 LSAW pipe for low-temperature pressure service. Available grades CC60, CC65, CC70, multiple classes, full NDT test, custom coating & cutting. Request MTC and quotation.
Related: ASTM A672 LSAW Steel Pipe, LSAW Pipe