| Standard | ASTM A671/A671M-20(2025) |
| Material | Carbon steel or alloy steel |
| Process | EFW |
| Grade | CA55, CB60, CB65, CB70, CC60, CC65, CC70, CD70, CD80, CFA65, CFB70, CFD65, CFE70, CG100, CH115, CJA115, CJB115, CJE115, CJF115, CJH115, CJP115, CK75,and CP85 |
| Class | 10, 11, 12, 13, 20, 21, 22, 23, 30, 31, 32, 33, 40, 41, 42, 43, 50, 51, 52, 53, 70, 71, 72, and 73 |
| Dimension | 16 in. [400 mm] in outside diameter or larger and of 1/4 in. [6 mm] wall thickness or greater |
| Application | Suitable for high-pressure service at atmospheric and Iower temperatures. |
What is ASTM A671/A671M LSAW Steel Pipe
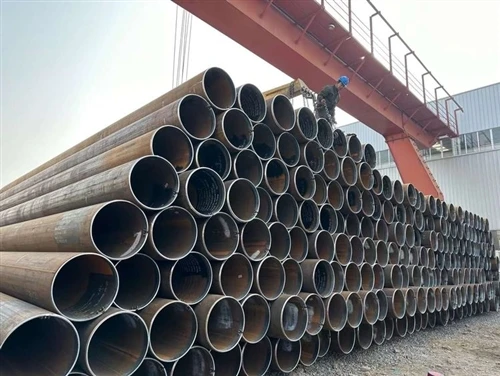
ASTM A671 is a steel pipe specification made from several analyses and strength levels of pressure vessel quality plates, manufactured through the electric-fusion-welded (EFW) process, suitable for high-pressure service at atmospheric or low temperatures.
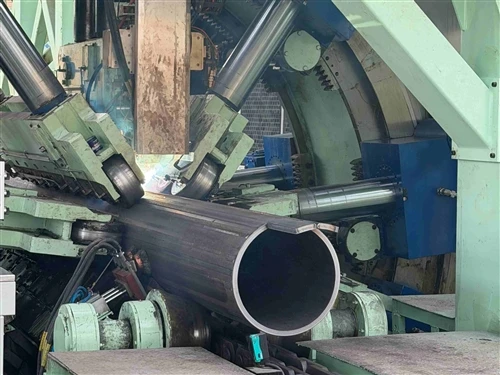
Electric fusion welding (EFW) is a process in which an electric arc is used to heat and melt metal in order to achieve a weld. EFW process has the advantages of fast welding speed, high welding quality, and a small heat-affected zone, which is especially suitable for welding thick-walled or large-diameter steel pipes.
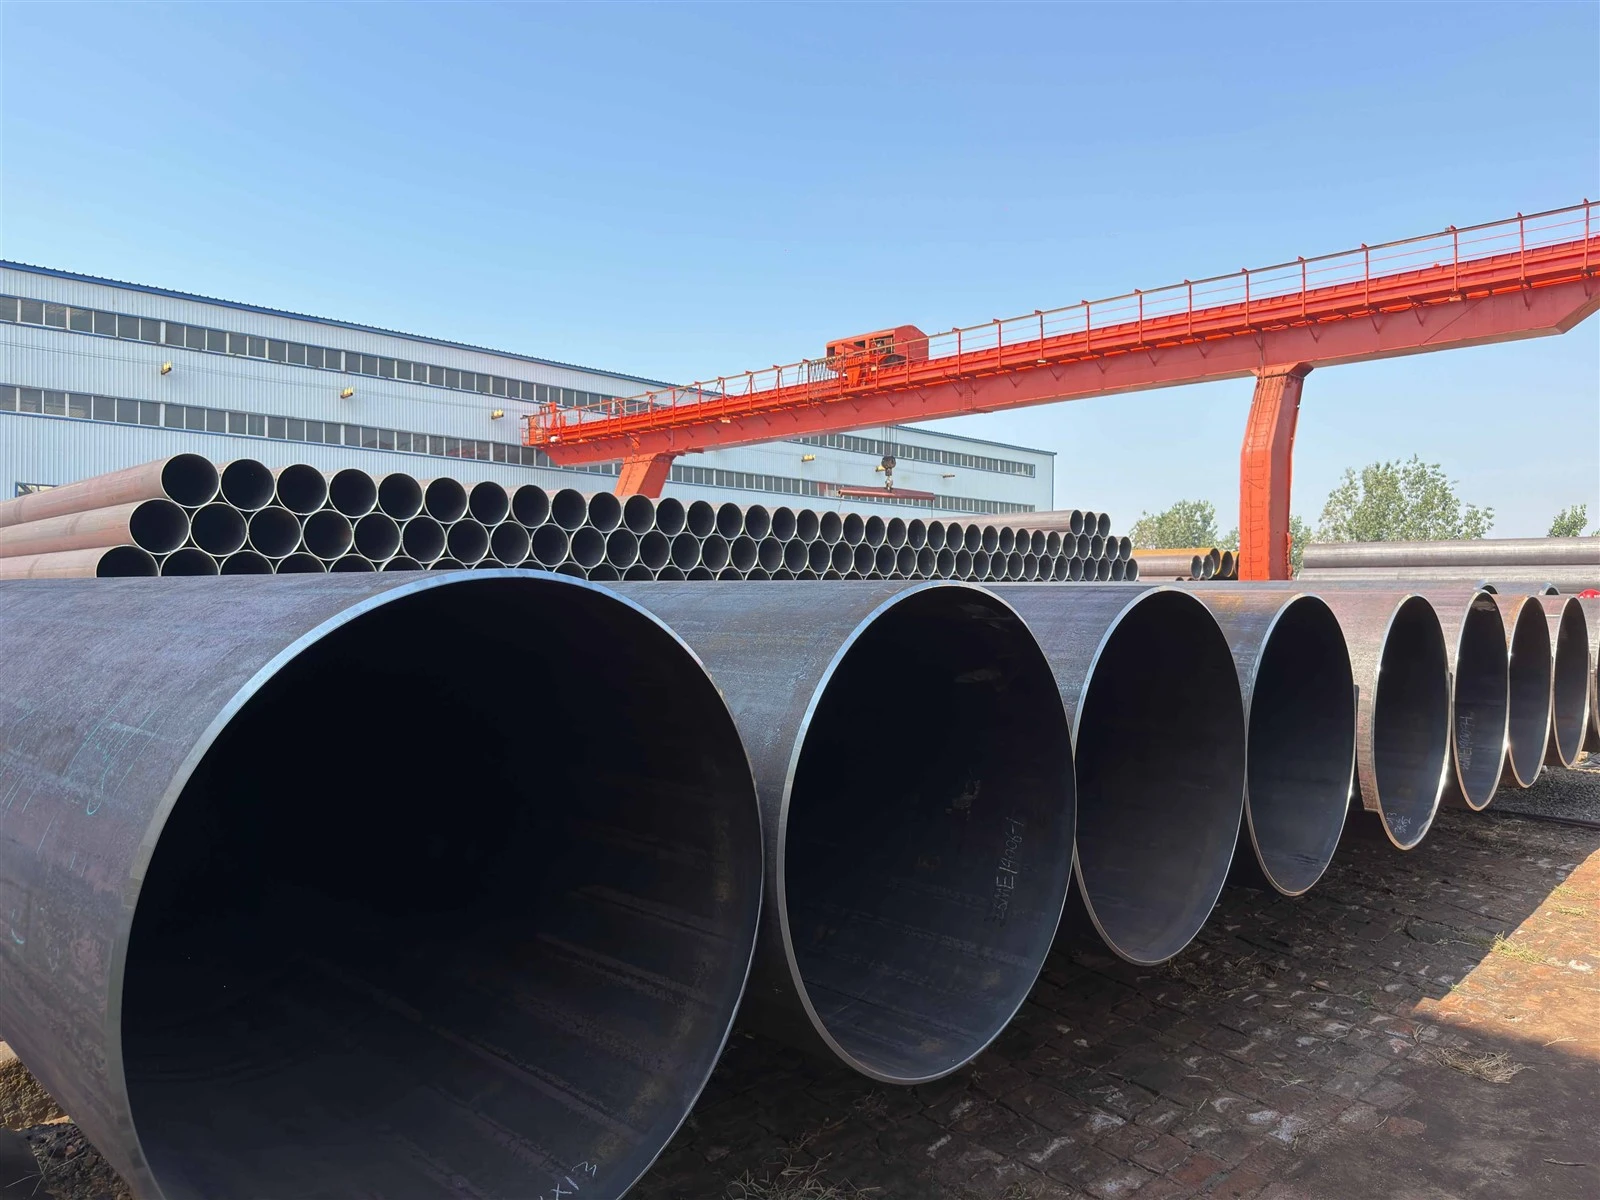
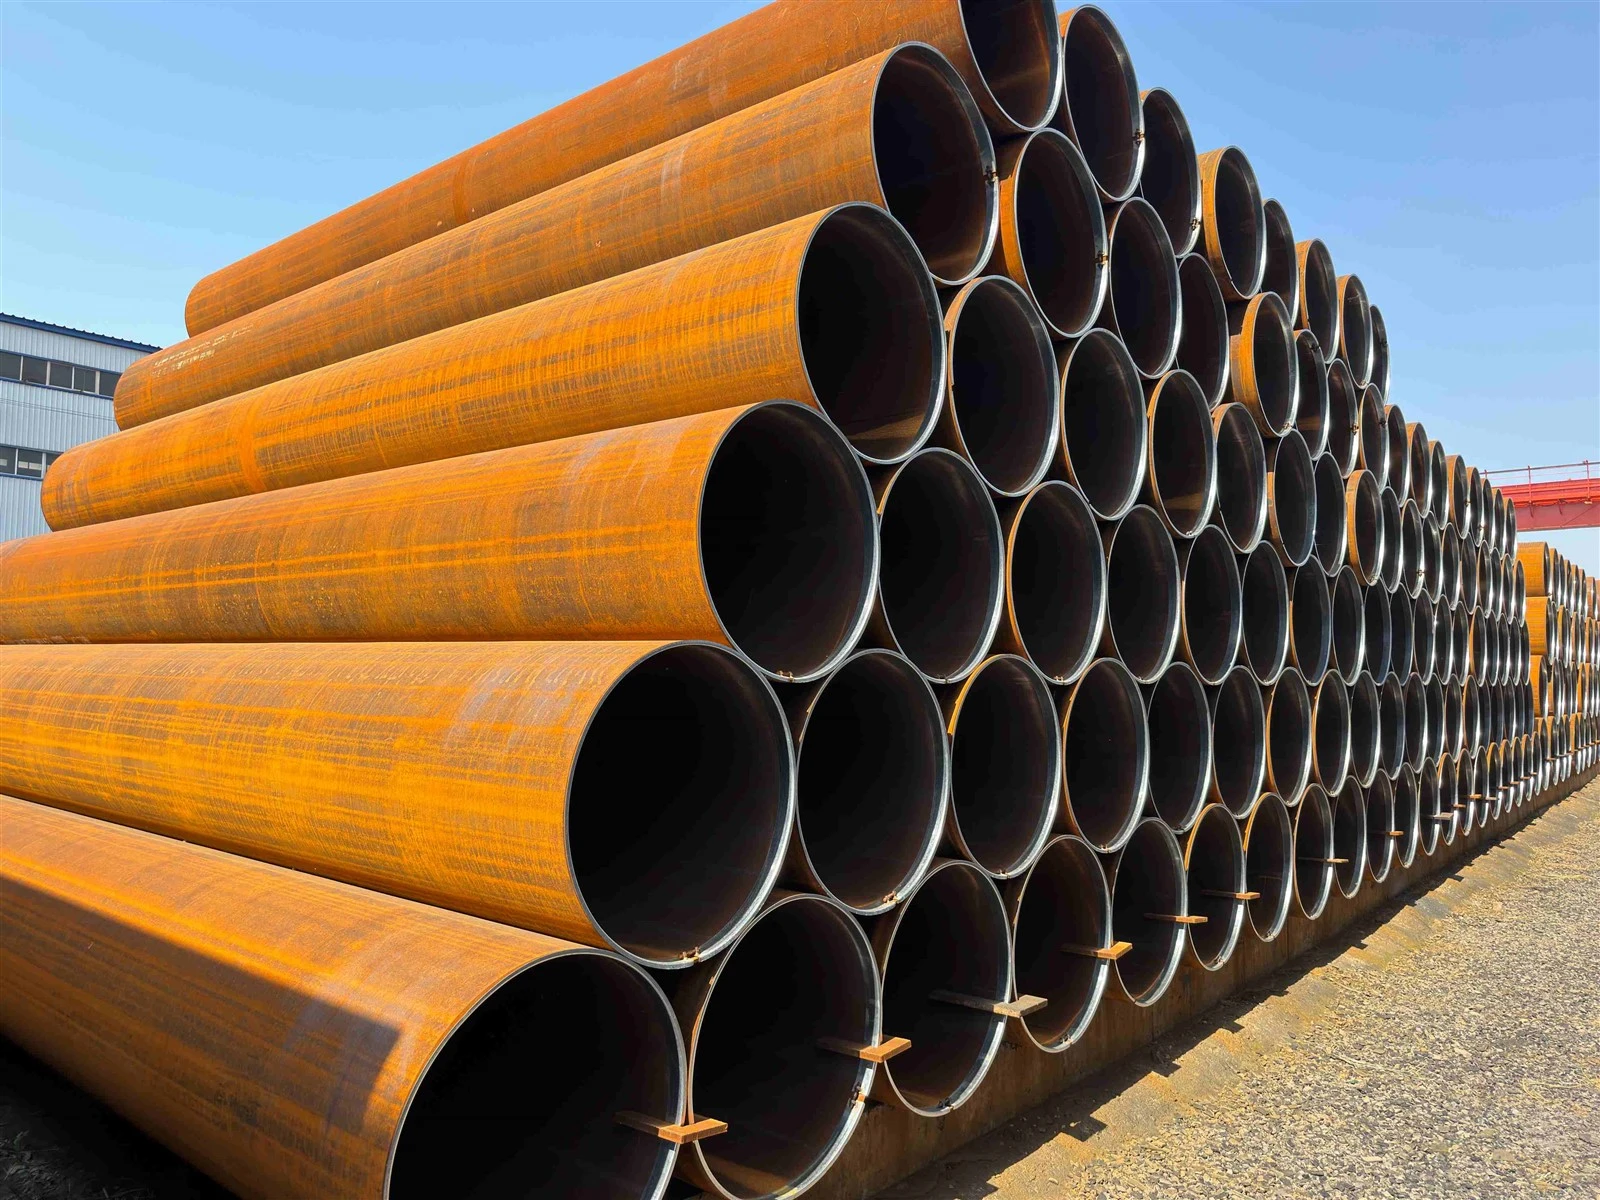
Dimension
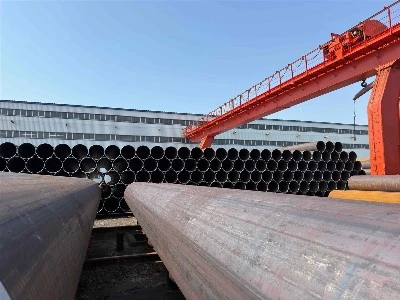
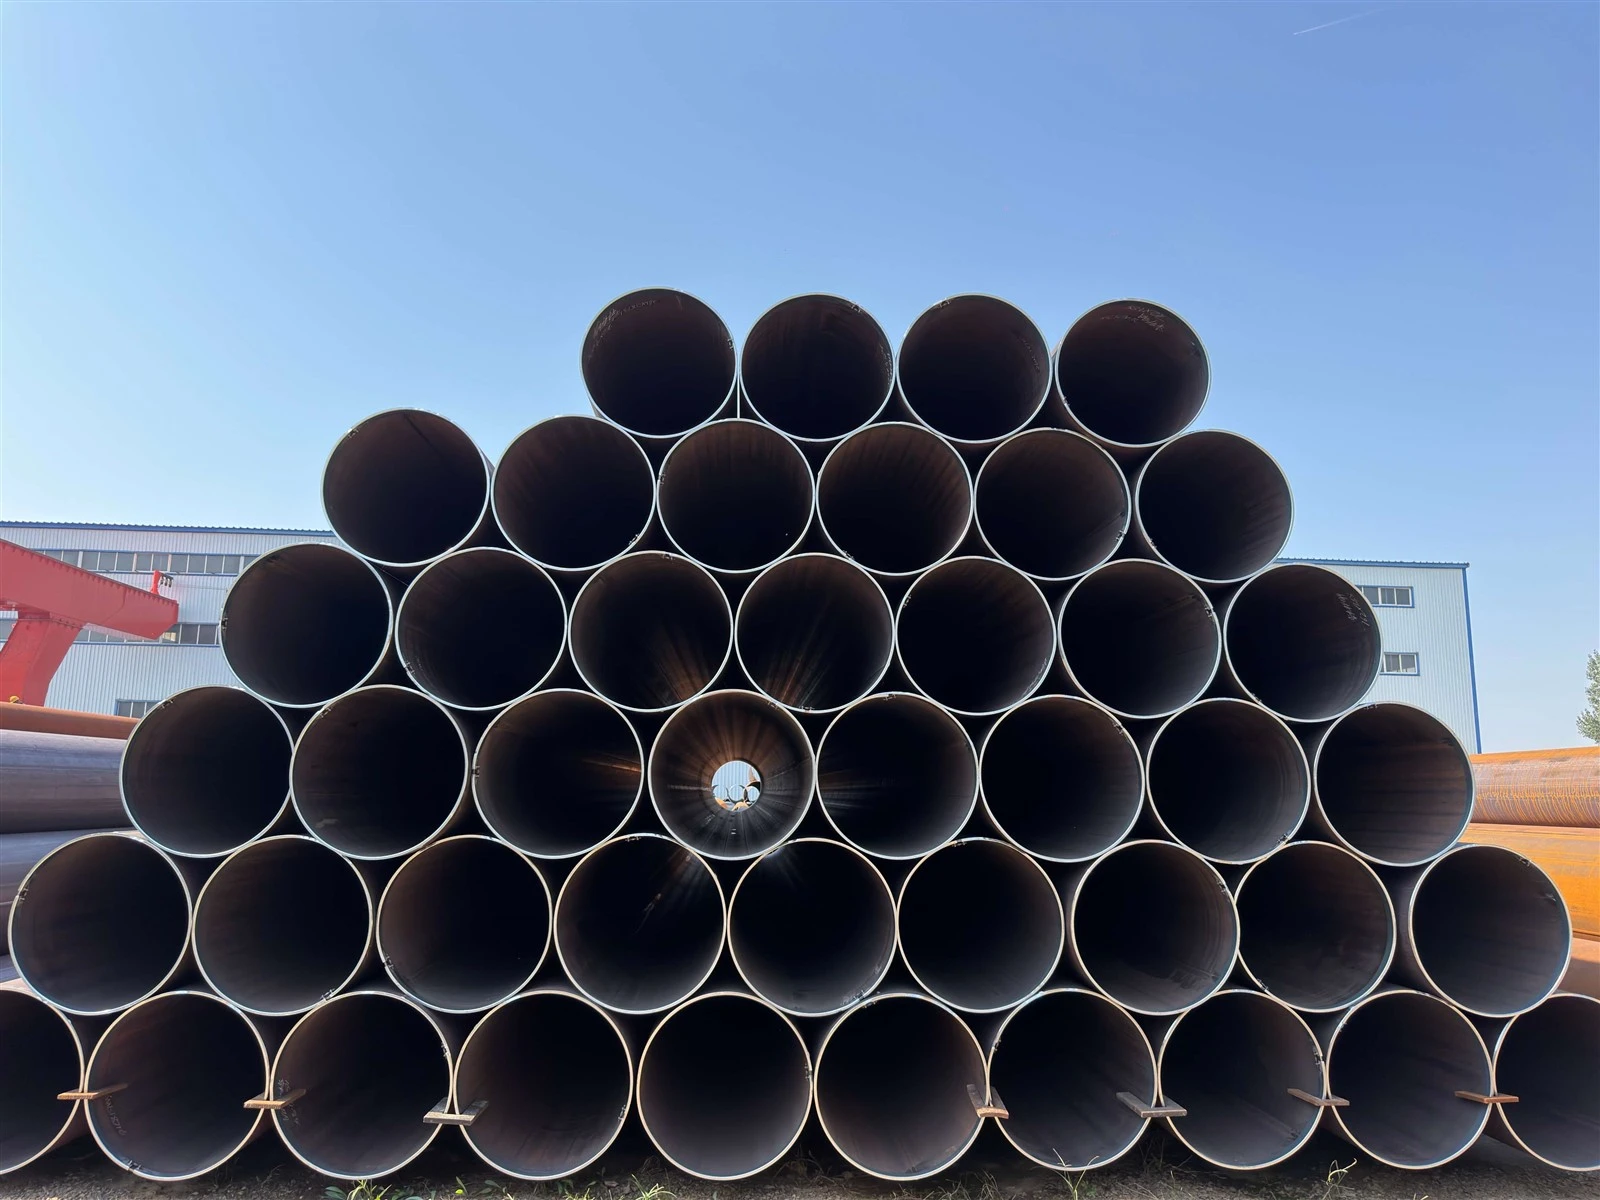
ASTM A671 dimensions generally include the following ranges:
- Outside diameter: 16 in. [400 mm] or larger;
- Wall thickness: 1/4 in. [6 mm] or greater;
Other sizes of tubing can be supplied on request, provided they meet other applicable requirements.
Dimension Tolerance
| Dimension | Tolerance |
| Outside Diameter | Based on circumferential measurement ±5 % of specified outside diameter |
| Out-of-Roundness | Difference between major and minor outside diameters, 1 % |
| Alignment | Using a 10 ft [3 m] straight edge placed so that both ends are in contact with the pipe, 1/8 in. [3 mm] |
| Thickness | Minimum wall thickness not more than 0.01 in. [0.3 mm] under |
| Lengths | Lengths with unmachined ends shall be within 0 – +0.5 mm [0 – +13 mm] of that specified |
Grade Classification
When you purchase ASTM A671 steel pipe, providing the specific Grade and Class to the supplier can clearly express the specific needs for the chemical composition, mechanical properties, manufacturing process, and testing requirements of the pipe.
ASTM A671 grades are determined by which standard and material of steel plate is used, including carbon steel, alloy steel, nickel steel, etc.
There are 23 grades. Below are the grades and the raw materials of the corresponding standard steel plates.
| Pipe Grade | Type of Steel | ASTM Specification | |
| No. | Grade/class/type | ||
| CA55 | plain carbon | A285/A285M | Gr C |
| CB60 | plain carbon, killed | A515/A515M | Gr 60 |
| CB65 | plain carbon, killed | A515/A515M | Gr 65 |
| CB70 | plain carbon, killed | A515/A515M | Gr 70 |
| CC60 | plain carbon, killed, fine-grain | A516/A516M | Gr 60 |
| CC65 | plain carbon, killed, fine-grain | A516/A516M | Gr 65 |
| CC70 | plain carbon, killed, fine-grain | A516/A516M | Gr 70 |
| CD70 | manganese-silicon, normalized | A537/A537M | Cl 1 |
| CD80 | manganese-silicon, quenched and tempered | A537/A537M | Cl 2 |
| CFA65 | nickel steel | A203/A203M | Gr A |
| CFB70 | nickel steel | A203/A203M | Gr B |
| CFD65 | nickel steel | A203/A203M | Gr D |
| CFE70 | nickel steel | A203/A203M | Gr E |
| CG100 | 9% nickel | A353/A353M | - |
| CH115 | 9% nickel | A553/A553M | Type 1 |
| CJA115 | alloy steel, quenched and tempered | A517/A517M | Gr A |
| CJB115 | alloy steel, quenched and tempered | A517/A517M | Gr B |
| CJE115 | alloy steel, quenched and tempered | A517/A517M | Gr E |
| CJF115 | alloy steel, quenched and tempered | A517/A517M | Gr F |
| CJH115 | alloy steel, quenched and tempered | A517/A517M | Gr H |
| CJP115 | alloy steel, quenched and tempered | A517/A517M | Gr P |
| CK75 | carbon-manganese-silicon | A299/A299M | Gr A |
| CP85 | alloy steel, age hardening, quenched and precipitation heat-treated | A736/A736M | Gr A, Class 3 |
For each grade of ASTM A671, the chemical composition and mechanical properties shall be in accordance with the requirements for the selection of steel plates.
Selection of materials should be made with attention to temperature of service. For such guidance. Specification A20/A20M may be consulted.
Listed below are some common grade materials, for grades not listed, you can contact us and our professional team is always at your service.
Class Classification & Heat Treatment
Class designates the type of heat treatment performed during the manufacture of the pipe, whether the weld is radiographically examined, and whether the pipe has been pressure tested.
| Class | Heat treatment on pipe | Radiography, see note: | Pressure test, see note: |
| 10 | none | none | none |
| 11 | none | 9 | none |
| 12 | none | 9 | 8.3 |
| 13 | none | none | 8.3 |
| 20 | stress relieved, see 5.3.1 | none | none |
| 21 | stress relieved, see 5.3.1 | 9 | none |
| 22 | stress relieved, see 5.3.1 | 9 | 8.3 |
| 23 | stress relieved, see 5.3.1 | none | 8.3 |
| 30 | normalized, see 5.3.2 | none | none |
| 31 | normalized, see 5.3.2 | 9 | none |
| 32 | normalized, see 5.3.2 | 9 | 8.3 |
| 33 | normalized, see 5.3.2 | none | 8.3 |
| 40 | normalized and tempered, see 5.3.3 | none | none |
| 41 | normalized and tempered, see 5.3.3 | 9 | none |
| 42 | normalized and tempered, see 5.3.3 | 9 | 8.3 |
| 43 | normalized and tempered, see 5.3.3 | none | 8.3 |
| 50 | quenched and tempered, see 5.3.4 | none | none |
| 51 | quenched and tempered, see 5.3.4 | 9 | none |
| 52 | quenched and tempered, see 5.3.4 | 9 | 8.3 |
| 53 | quenched and tempered, see 5.3.4 | none | 8.3 |
| 70 | quenched and precipitation heat-treated | none | none |
| 71 | quenched and precipitation heat-treated | 9 | none |
| 72 | quenched and precipitation heat-treated | 9 | 8.3 |
| 73 | quenched and precipitation heat-treated | none | 8.3 |
Note: All references in the table have been listed below and you can review them as needed.
Heat Treatment
5.3.1 Classes 20, 21, 22, and 23 pipes shall be uniformly heated within the post-weld beat-treatment temperature range indicated in Table 2 for a minimum of 1 h/in. [0.4 h/cm] of thickness or for 1 h. whichever is greater.
5.3.2 Classes 30, 31, 32, and 33 pipes shall be uniformly heated to a temperature in the austenitizing range and not exceeding the maximum normalizing temperature indicated in Table 2 and subsequently cooled in the air at room temperature.
5.3.3 Classes 40, 41, 42, and 43 pipes shall be normalized in accordance with 5.3.2. After normalizing, the pipe shall be reheated to the tempering temperature indicated in Table 2 as a minimum and held at temperature for a minimum of 1/2 h/in. [0.2 h/cm] of thickness or for 1/2 h, whichever is greater, and air-cooled.
5.3.4 Classes 50, 51, 52, and 53 pipes shall be uniformly heated to a temperature in the austenitizing range, and not exceeding the maximum quenching temperature indicated in Table 2 and subsequently quenched in water or oil. After quenching, the pipe shall be reheated to the tempering temperature indicated in Table 2 as a minimum and held at that temperature for a minimum of 1/2 h/in. [0.2 h/cm] of thickness or for 1/2 h, whichever is greater, and air-cooled.
| ASTM A671 Table 2 Heat Treatment Parameters | |||||
|---|---|---|---|---|---|
| Pipe grade | Post-weld heat treat temp range, °F [°C] | Max normalizing temp, °F [°C] | Min quenching temp, °F [°C] | Tempering temp, °F [°C] | Precipitation heat treat temp range, °F [°C] |
| CA55 | 1100-1250 [590-680] | 1700 [925] | - | - | - |
| CB60 | 1100-1250 [590-680] | 1750 [950] | - | - | - |
| CB65 | 1100-1250 [590-680] | 1750 [950] | - | - | - |
| CB70 | 1100-1250 [590-680] | 1750 [950] | - | - | - |
| CC60 | 1100-1200 [590-650] ᶜ | 1700 [925] | 1700 [925] | 1100 [590] ᴰ | - |
| CC65 | 1100-1200 [590-650] ᶜ | 1700 [925] | 1700 [925] | 1100 [590] ᴰ | - |
| CC70 | 1100-1200 [590-650] ᶜ | 1700 [925] | 1700 [925] | 1100 [590] ᴰ | - |
| CD70 | 1100-1250 [590-680] | 1700 [925] | - | - | - |
| CD80 | 1100-1250 [590-680] ᶜ | - | 1650 [900] | 1100 [590] | - |
| CFA65 | 1100-1175 [590-635] | 1750 [950] | - | - | - |
| CFB70 | 1100-1175 [590-635] | 1750 [950] | - | - | - |
| CFD65 | 1100-1175 [590-635] | 1750 [950] | - | - | - |
| CFE70 | 1100-1175 [590-635] | 1750 [950] | - | - | - |
| CG100 | 1025-1085 [550-580] | 1650 ± 25 [900 ± 15] plus ᴱ | - | 1050-1125 [560-605] | - |
| CH100 | 1025-1085 [550-580] | 1450 ± 25 [790 ± 15] | 1475-1700 [800-925] | 1050-1175 [560-635] ᴲ | - |
| CJA115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CJB115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CJE115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CJF115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CJH115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CJP115 | 1000-1100 [540-590] | - | 1650-1725 [900-940] | 1150 [620] | - |
| CK75 | 1100-1250 [590-680] | 1700 [925] | - | - | - |
| CP85 | 1000-1175 [540-635] | - | 1725 [940] | - | 1000-1225 [540-665] |
|
B Numbers indicate minimum tensile strength in ksi. C In no case shall the post-weld heat treatment temperature exceed the mill tempering temperature. D Tempering range 1100-1300 [590-705], if accelerated cooling utilized per specification A516/A516M. E If hot forming is performed after heating to a temperature in a range from 1650-1750 [900-955], the first normalize may be omitted. F Prior to the tempering treatment, the plates may be subjected to an intermediate heat treatment consisting of heating to |
|||||
What We Can Supply?
Brisk Steel Factory manufactures ASTM A671 LSAW pipe for low-temperature pressure service. Available grades CC60, CC65, CC70, multiple classes, full NDT test, custom coating & cutting. Request MTC and quotation.
Related: ASTM A671 LSAW Steel Pipe, LSAW Pipe