

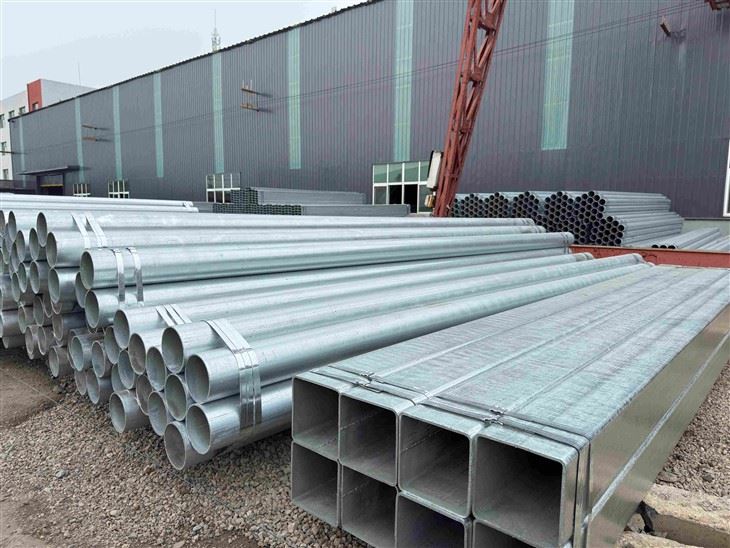
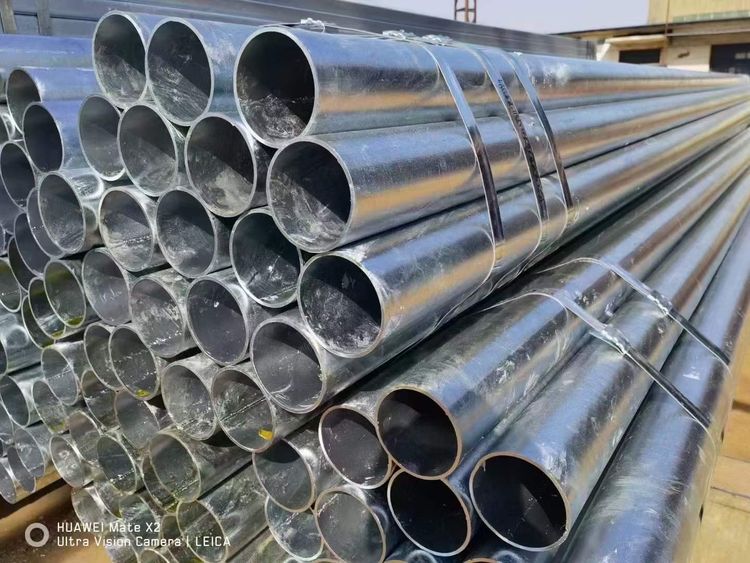
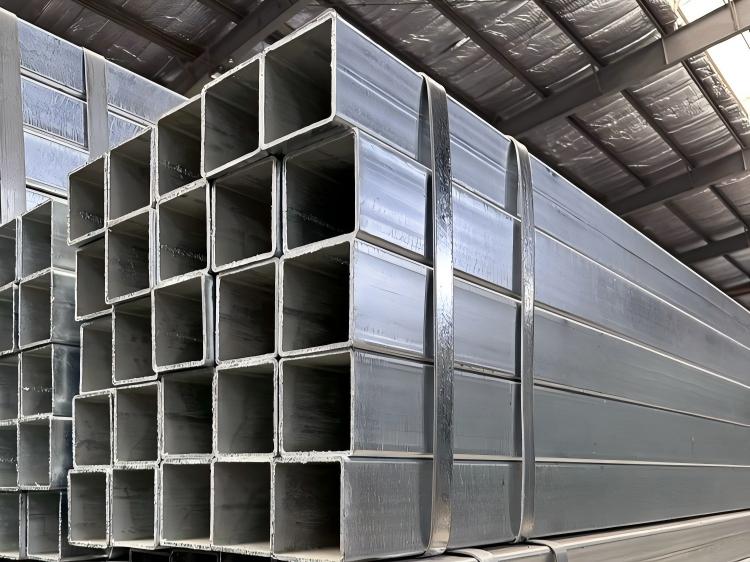
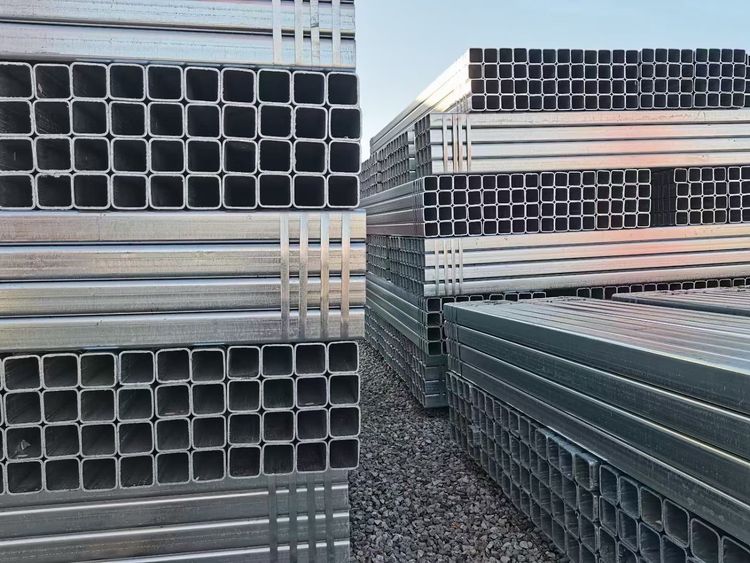
Tianjin Brisk Metalwork Co., Ltd. is one of the leading manufacturers and suppliers of hot dip galvanized s275 hollow section in China. We have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy bulk durable hot dip galvanized s275 hollow section from our factory.
What Happens to S275 Steel at Zinc-Bath Temperature?
Hot-dip galvanizing runs the finished section through molten zinc at roughly 450 degC, well below the temperatures used for normalizing or heat treatment. For straight, un-strained sections, this exposure has no meaningful effect on yield strength or toughness - the dip time is short and the temperature is nowhere near what is needed to alter the steel's microstructure.
The exception is the cold-formed corner. On EN 10219 cold-formed S275 hollow section, the four corners of a square or rectangular profile are bent to a tight radius - typically around 2x the wall thickness - which locks a significant amount of strain hardening into the steel at exactly that point. Reheating strained steel in that condition, even briefly and at a moderate temperature like a zinc bath, can trigger strain-age embrittlement: a measurable drop in impact toughness concentrated right at the corner, which is also usually the most highly stressed point in a welded or bolted connection.
Why Does This Matter More on S275 Than It Sounds Like It Should?
This is not a defect in the material - it is a known interaction between cold-forming and subsequent heat exposure, and it is manageable, but only if it is controlled rather than ignored:
- Corner bend radius control during forming keeps strain concentration within the range the standard allows, rather than pushing toward the tightest radius the mill can physically produce.
- Chemistry control on the coil - particularly keeping silicon within a band that avoids the reactive-steel zone - reduces the metallurgical interaction between the zinc and the strained corner surface during the dip.
- Where the specification calls for it, sourcing pre-normalized coil relieves the cold-work strain before forming, so the corner is not carrying peak hardening into the bath at all.
We flag this specifically on S275 hollow section orders with wall thickness above roughly 8mm going into galvanized structural connections - at that thickness, corner toughness after galvanizing is worth a conversation before the order is confirmed, not a surprise during third-party testing.
What Do We Control on Every Galvanized S275 Batch?
- Surface preparation - degreasing, acid pickling, and fluxing before dip, so coating adhesion isn't compromised by mill scale or oil residue.
- Coating mass verified against EN ISO 1461's thickness-based requirement, with heavier-wall sections held to a proportionally thicker coating specification than thin-wall material.
- Corner sampling for post-galvanizing toughness on structural orders where the buyer specifies it, pulled from the same batch and corner location that carries the design stress.
- Venting and drainage confirmed before dip on closed sections, since trapped air or moisture at dip temperature is a separate and unrelated risk to the corner embrittlement issue above.
- Withdrawal speed and drainage control to avoid zinc pooling at internal corners, which affects appearance and localized coating thickness rather than the steel itself.
Case in point
thickness 10mm, for a galvanized roof-truss system with bolted corner connections. The buyer's spec called out impact toughness testing after galvanizing - a requirement the original mill contact hadn't flagged before rolling. Post-galvanizing Charpy samples taken from the corner region came back below the required minimum at two of six test points, traced to a tight 1.5x-wall-thickness bend radius combined with standard-chemistry coil that hadn't been screened for strain-age sensitivity. The batch was reworked with a wider 2.5x radius reform on the next run and pre-normalized coil, adding 6 days to the production schedule but clearing toughness testing on every subsequent sample. Since then, we ask every buyer specifying post-galvanizing toughness testing to confirm it at quote stage, not after the first batch fails.
Related:S275 Structural Hollow Section
FAQ
Q: Does galvanizing change the yield strength of S275 hollow section?
A: No - away from cold-formed corners, the zinc bath temperature is too low and the exposure too short to alter the base material's yield or tensile properties.
Q: Can you supply hot-dip galvanized S275 under EN 10210 instead of EN 10219?
A: Yes - hot-finished EN 10210 material does not carry the same cold-work strain at the corners, since it's normalized after forming, so it avoids this specific consideration. Tell us which route your specification requires.
Q: What coating thickness should I expect on a standard order?
A: Coating mass scales with wall thickness under EN ISO 1461 rather than being a single fixed number across all sizes - send us your section dimensions and we'll confirm the applicable coating class.
Q: Do you offer post-galvanizing impact testing as standard, or only on request?
A: It's available on request rather than run by default on every batch - specify it when you place the order so we can pull samples from the correct location and thickness.


Hot Tags: hot dip galvanized s275 hollow section, China hot dip galvanized s275 hollow section manufacturers, suppliers, factory


