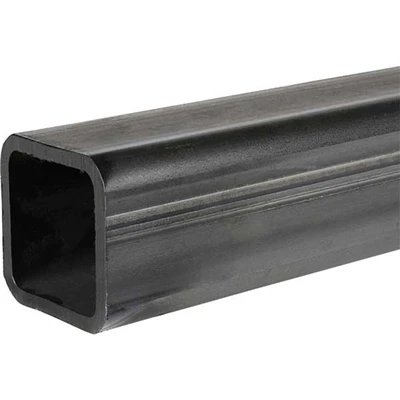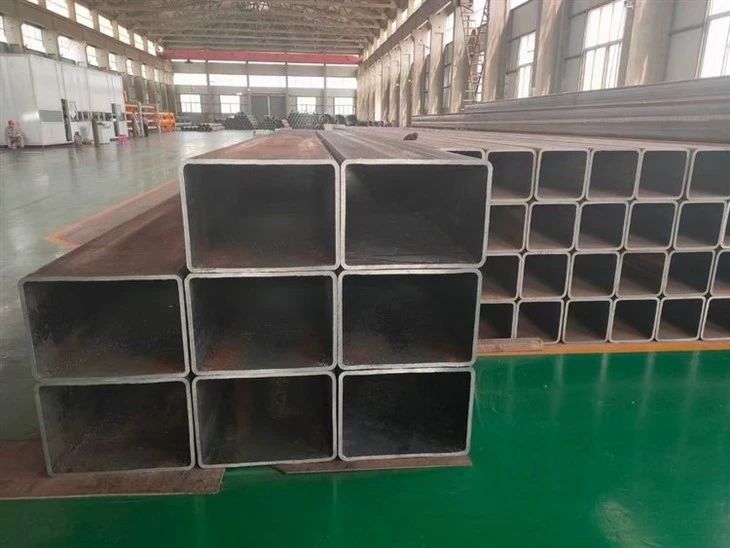
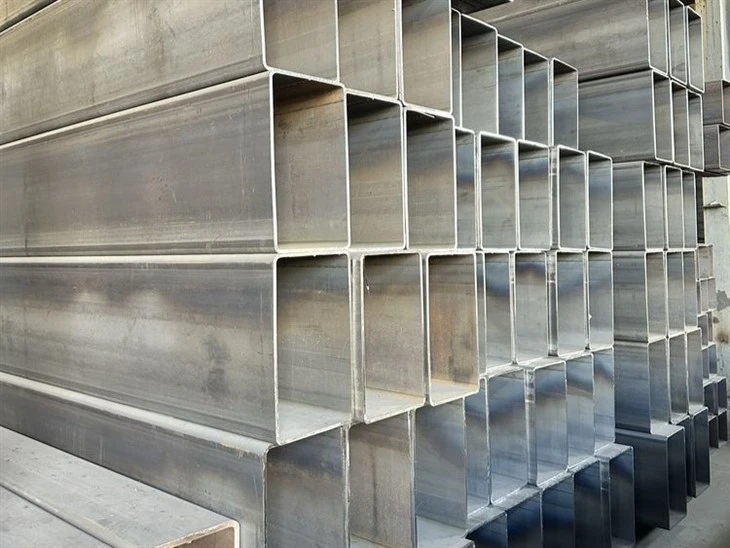
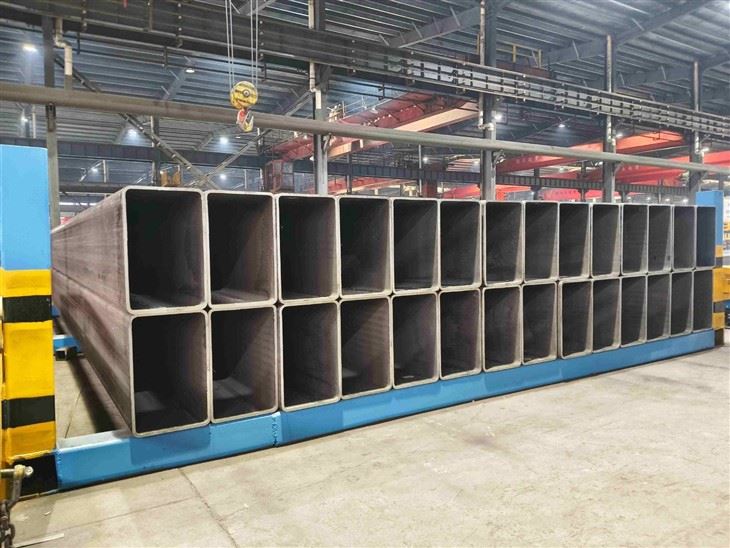
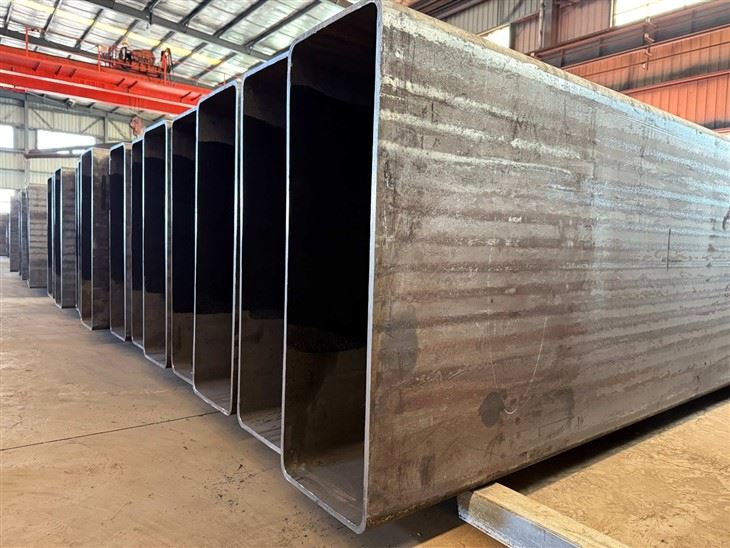
Tianjin Brisk Metalwork Co., Ltd. is one of the leading manufacturers and suppliers of en 10219 rectangular hollow section in China. We have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy bulk durable en 10219 rectangular hollow section from our factory.
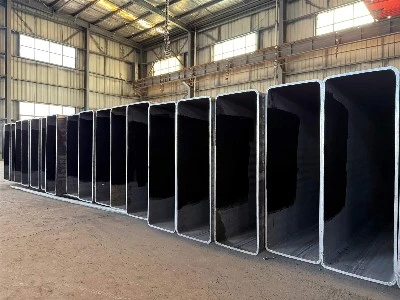
What Do We Supply Under EN 10219 Rectangular Hollow Section?
Size range: 10x20mm to 600x400mm , redrawn to1000×1500mm. Wall thickness: 1.2mm to 20mm. Standard lengths: 6m and 12m, custom lengths on request.
Grades supplied: S235JRH, S275J0H/J2H, S355J0H/J2H/K2H, S460NH. Aspect ratios (width-to-height) from near-square up to 3:1 on standard tooling; higher ratios quoted on request. Surface finish: black mill finish, hot-dip galvanized, painted/primed. Every lot ships with an EN 10204 3.1 mill test report.
Why buyers order rectangular instead of square: an RHS carries a higher moment of inertia on its strong axis than a square section of the same steel weight, because the material is placed further from the neutral axis on that side. For beams and one-directional bending members, this means more stiffness per kilogram of steel - the load runs one way, so the section is built to resist that direction harder than the other. This is the reverse logic of our square section line, where both axes are made equal on purpose; here, we make them unequal on purpose.
How Do We Control the Aspect Ratio Through Cold-Forming?
The aspect ratio is set at the strip-slitting stage and held through forming - this is where we build accuracy in, not correct it after the fact.
- Strip width calculated and verified per target aspect ratio before it enters the mill - a strip cut for a 2:1 section cannot be corrected into a 1.5:1 section downstream.
- In-line dimension checks on both the wide face and the narrow face independently - we measure each face separately rather than relying on a single diagonal check, since a rectangular section can drift on one face without showing on the other.
- Face flatness monitored on the wider face - as aspect ratio increases, the wide face is more prone to slight bowing during forming; we hold this within a tight band because it affects both squareness at the corners and how cleanly the section seats against a base plate or connecting member.
Why Is Installation Orientation the Risk Point With RHS - and How Do We Reduce It?
A rectangular section only performs as designed when it is installed with its strong axis aligned to the load. Get the orientation wrong on site, and the section is carrying load on its weaker axis - which is not a defect in the steel, it is an error in how it went up.
A specific case: a steel-frame fabricator ordered 250x150x8mm RHS beams for a mezzanine floor designed to bend about the 250mm-deep axis. A batch delivered to a different site on the same project was installed rotated 90 degrees by a field crew unfamiliar with the drawing convention - the beams were carrying load on the shallow 150mm axis instead. The deflection under load exceeded the design limit by roughly 40 percent before the error was caught during a routine site inspection, and the affected run (approximately 60 meters of beam) had to be re-set. The steel was never at fault; the orientation was.
We reduce this risk two ways on our end:
- Directional marking on every length - each piece is stenciled to show the strong-axis face, not just the section size, so it is visually obvious on site which way the beam goes up.
- Packing lists cross-referenced to your drawing numbers on request, so beams for different structural roles in the same shipment do not get mixed on the yard.
What Applications Do We Supply RHS For Most Often?
- Beams and purlins - one-directional bending where a higher strong-axis stiffness at lower steel weight than an equivalent square section is the buying reason.
- Frame members with a known dominant load direction - portal frame rafters, crane runway supports, mezzanine edge beams.
- Facade and curtain wall mullions - where the deeper axis resists wind load and the shallower axis keeps the sightline narrow.
- Combined square-column-to-rectangular-beam frames - many of our orders pair SHS columns (see our square hollow section line) with RHS beams in the same frame, since the column needs no weak axis while the beam is deliberately built with one.
Can You Process RHS for Connection Work Before Shipment?
Yes - the same in-house processing available on our square line runs on rectangular sections.
- CNC plasma or laser cutting for copes, notches, and connection profiles from your DXF/DWG file.
- End-facing and beveling for butt-weld or flange-plate connections.
- Drilling and punching to your bolt-hole pattern for beam-to-column or base-plate connections.
- Web and flange-style stiffener cutting for beams landing on column faces at non-standard angles.
Send your fabrication drawing with the order and we quote processed pricing alongside raw tube pricing.
EN 10219 Rectangular Hollow Section - Standard Capability
| Item | Our Range |
|---|---|
| Size range | 10x20mm to 600x400mm / redrawn to1000×1500mm |
| Wall thickness | 1.2mm to 20mm |
| Aspect ratio (standard tooling) | Up to 3:1; higher on request |
| Standard length | 6m / 12m (custom on request) |
| Grades | S235JRH, S275J0H/J2H, S355J0H/J2H/K2H, S460NH |
| Surface finish | Black, hot-dip galvanized, painted/primed |
| Processing | CNC cutting, coping, end-facing, drilling |
| Certification | EN 10204 3.1, mill test report per lot |
FAQ
Q: Do you mark which face is the strong axis on delivery, or do we have to check the drawing every time?
A: Every length is stenciled to identify the strong-axis face, not only the nominal section size, so the orientation is visible on the yard without pulling the drawing for each piece.
Q: Can we order a non-standard aspect ratio, or are we limited to your listed sizes?
A: Standard tooling covers ratios up to 3:1 without lead-time impact. Higher ratios or sizes between our listed tooling steps are quoted individually - send us the target dimensions and we confirm feasibility and lead time before you commit.
Q: Can one shipment mix RHS beams and SHS columns for the same frame?
A: Yes - this is one of our more common order patterns. Provide the quantity split by section and size and we consolidate into one shipment with cross-referenced packing lists if you need beams and columns kept traceable to specific drawing zones.
Q: Does a higher aspect ratio section cost more per ton than a near-square RHS?
A: Not inherently - cost scales mainly with wall thickness and total steel weight, not ratio. What does change with higher ratios is tooling availability at certain size steps, which is why we confirm feasibility on non-standard ratios before quoting rather than pricing blind.


Hot Tags: en 10219 rectangular hollow section, China en 10219 rectangular hollow section manufacturers, suppliers, factory